Setting realistic die-cut tolerances for soft foam and thin film parts starts with understanding how the material behaves under cutting pressure and which process will be used. Over-constraining a drawing with machined-metal tolerances drives cost and scrap without improving function. This article explains how to specify tolerances that are manufacturable and meaningful.
Why Soft Foam and Thin Film Need Different Tolerance Logic
Soft foam and thin film do not behave like rigid metal or plastic. Foam compresses under die pressure and can spring back after cutting, so a dimension measured immediately after cutting may differ from one measured hours later. Thin films can stretch, wrinkle, or shift during web handling, especially when the film is below 0.05 mm thick. These behaviors mean the tolerance must account for material recovery and process variation, not just tool accuracy.
A flatbed die cutter applies uniform vertical force across the die, which helps control compression in thicker foam. Rotary die cutting uses continuous rolling pressure and is better suited to high-volume thin film parts, but web tension and film modulus affect dimensional stability. The same nominal dimension can require a different tolerance depending on the process selected.[1] [2]
- Foam thickness can vary by ±10% or more depending on grade and supplier.
- Thin films below 0.05 mm are sensitive to tension and may require wider tolerances.
- Material recovery after cutting can change dimensions by several percent for soft foams.
Process Capability: Rotary vs. Flatbed Die Cutting
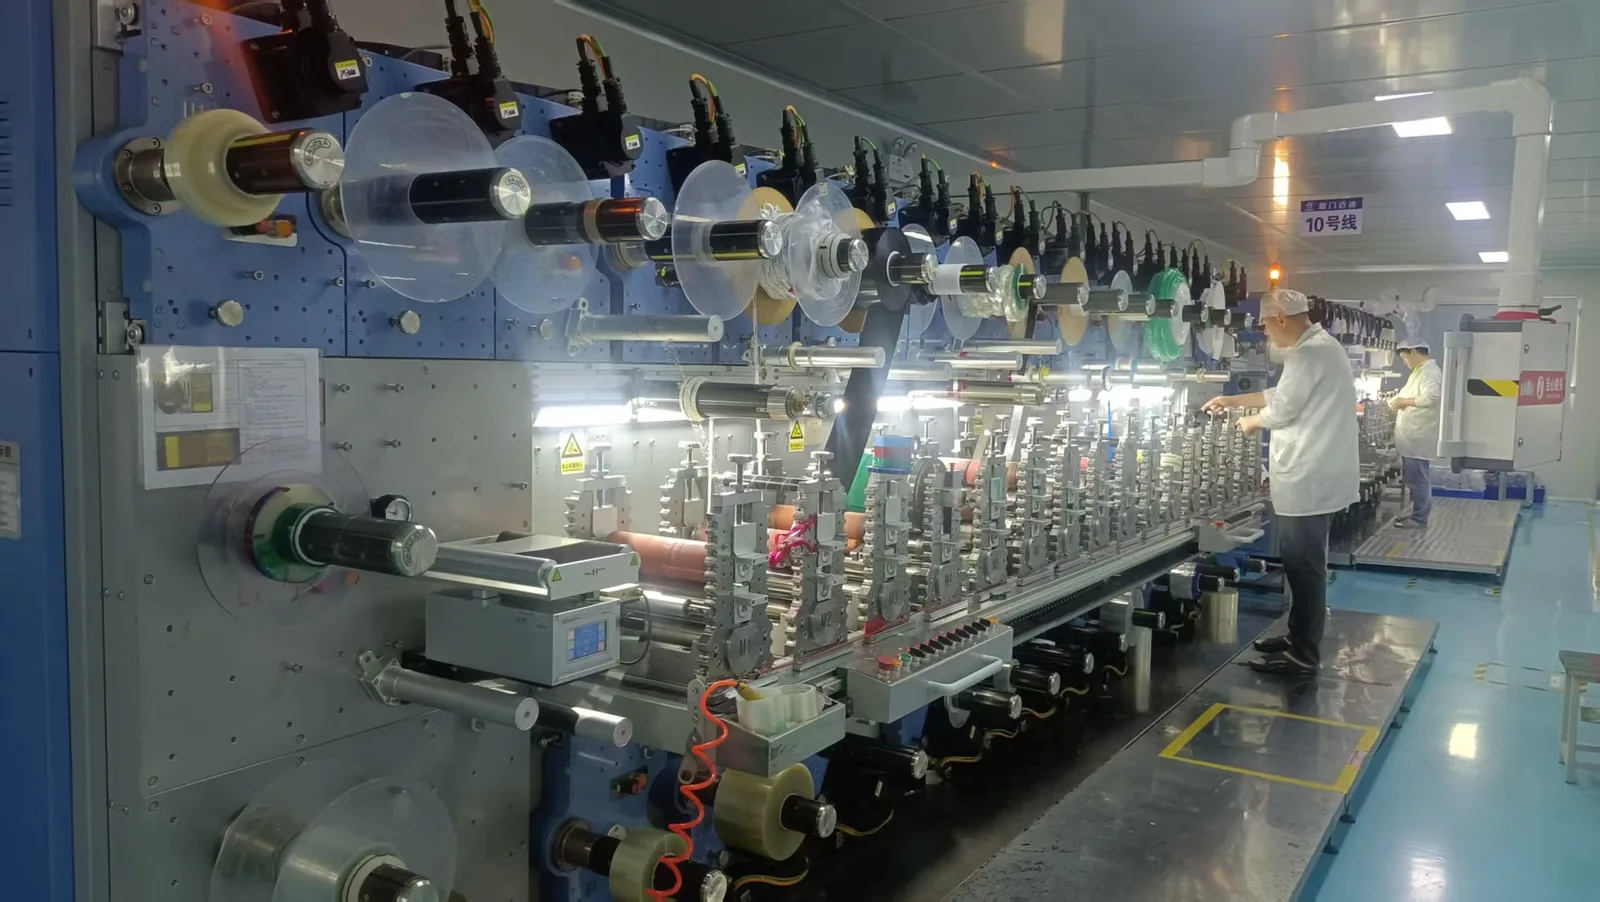
Rotary die cutting is a continuous process where a cylindrical die cuts against an anvil roll. It is fast and repeatable for long runs, but the achievable tolerance depends on web speed, tension control, and die condition. Flatbed die cutting uses a hydraulic or electric press to stamp the die into the material. It offers more control for thick or compressible materials and is often used for prototypes and short runs.[1] [2]
For a given part, rotary cutting may hold a tighter tolerance on length along the web direction than on width, because web tension affects the cross-web dimension. Flatbed cutting can hold consistent dimensions across the entire part area but is slower. The choice between processes should be made before the tolerance is locked on the drawing.
- Rotary: high speed, good for thin films, tolerance affected by web tension.
- Flatbed: better for thick foam, uniform pressure, lower tooling cost for short runs.
- Laser cutting is an option for very complex shapes but has different edge effects.
Material Behavior and Dimensional Stability
Soft foam, such as polyurethane or polyethylene, is viscoelastic. It compresses under the die and then partially recovers. The amount of recovery depends on foam density, cell structure, and time. A dimension measured immediately after cutting may be smaller than the final relaxed dimension. Thin films, especially polyester or polyimide, can be dimensionally stable but may curl or distort if adhesive liners are removed.
When specifying a tolerance, state the measurement condition: time after cutting, temperature, and whether the part is on the liner or free. Without this, the supplier and customer may measure the same part differently and disagree on acceptance.
- Specify measurement time after cutting (e.g., 24 hours at 23°C).
- State whether dimensions are measured on the liner or free state.
- For foam, consider a relaxation period before final inspection.
Drawing Tolerance Stack and Datum Selection
A die-cut part drawing often has multiple features: overall length, width, hole positions, and edge distances. If each feature is dimensioned from a different edge, the tolerance stack can exceed the functional requirement. Use a common datum scheme, such as two perpendicular edges or a centerline, to reduce accumulation.[3] [4]
For example, if a hole is located 10 mm from the left edge and another hole is located 10 mm from the right edge, the distance between holes depends on the overall width tolerance. Dimensioning both holes from the same edge removes that dependency. This is standard tolerance stack practice and applies directly to die-cut parts.[3]
- Use a common datum edge or centerline for all critical features.
- Avoid chain dimensioning for features that must align with mating parts.
- Consider GD&T profile tolerances for complex shapes.
First Article Inspection and Validation Protocol
First article inspection (FAI) verifies that the production process can meet the drawing tolerance. For soft foam and thin film, FAI should include measurements at multiple time points to capture relaxation or dimensional drift. A practical protocol is to measure immediately after cutting, after 24 hours, and after any required environmental conditioning.
The FAI report should record the measurement method, including whether a vision system, caliper, or optical comparator was used. For thin films, non-contact measurement is preferred to avoid deforming the part. The report should also note the liner condition and part orientation during measurement.
- Measure at T0, T+24h, and after conditioning.
- Use non-contact measurement for films below 0.1 mm.
- Record liner presence and part orientation.
Decision Matrix: Selecting Tolerance Class by Material and Process
The following matrix is a design-screening aid, not a universal specification. It combines material family, thickness, and cutting process to suggest a starting tolerance class. Final tolerances must be confirmed with the exact grade and validated by first article inspection.
For soft foam above 3 mm thickness cut on a flatbed, a typical starting tolerance is ±0.5 mm. For thin film below 0.1 mm cut on a rotary line, a starting tolerance of ±0.25 mm is often achievable, but web tension and film modulus can widen this. These are representative ranges across material families FLEXCEND can source and convert; they are not guaranteed finished-part values.
- Soft foam >3 mm, flatbed: start at ±0.5 mm.
- Thin film <0.1 mm, rotary: start at ±0.25 mm.
- Adhesive laminates: add liner tolerance and adhesive squeeze-out allowance.
Drawing Inputs That Make a FLEXCEND Review Useful
A drawing review is most productive when it includes the material specification, adhesive stack, liner type, and the functional requirement for each dimension. Mark critical dimensions that affect assembly fit or performance, and indicate which dimensions can use a looser tolerance. This allows the converter to propose a process and tolerance that balances cost and capability.
Include the part orientation on the roll or sheet, any pull-tab or liner extension requirements, and the expected volume. These details affect tooling design and process selection, which in turn influence the achievable tolerance.
- Material grade and thickness with supplier datasheet.
- Adhesive type and liner specification.
- Critical vs. non-critical dimensions.
- Expected annual volume and delivery format.
What to send for a useful review
- Material grade, thickness, and supplier datasheet
- Adhesive stack and liner type
- Cutting process preference (rotary, flatbed, laser) or open to recommendation
- Critical dimensions and functional requirements
- Datum scheme and tolerance stack analysis
- Measurement method and time after cutting
- Environmental conditioning requirements
- Expected annual volume and delivery format
- Any pull-tab or liner extension needs
- First article inspection requirements
Questions teams ask during selection
What is a realistic tolerance for die-cut soft foam?
For foam thicker than 3 mm cut on a flatbed, a starting tolerance of ±0.5 mm is common. Thinner or denser foams may hold tighter, but material recovery and measurement time must be specified.
Can thin film parts hold ±0.1 mm?
Some thin films can hold ±0.1 mm on a rotary line if web tension is well controlled and the film is dimensionally stable. However, films below 0.05 mm often require ±0.25 mm or more due to handling distortion.
How does rotary die cutting affect tolerance compared to flatbed?
Rotary cutting is faster and can be very repeatable in the machine direction, but cross-web dimensions may vary with tension. Flatbed cutting provides uniform pressure and is often better for thick or compressible foam.[1] [2]
Should I specify tolerance on the liner or free state?
Specify the measurement condition explicitly. For adhesive parts, dimensions are usually measured on the liner to avoid distortion. For foam, a free-state measurement after relaxation may be more representative.
What should be included in a first article inspection for die-cut parts?
FAI should include measurements at multiple time points, the measurement method, liner condition, and part orientation. Non-contact measurement is preferred for thin films.
Sources and technical references
References support the published context and cited data. Final material and assembly decisions still require grade-specific documentation and application validation.
- Understanding Flatbed Die Cutting Machines in 3 Minutes | Yicheenyicheen.com · Accessed
- Die Cutting Services: Rotary & Flat Bed Solutionscgstape.com · Published · Accessed
- Tolerance Stack Up Analysis - Cheat Sheetrd8.tech · Accessed
- How Tolerance Stack-Up Impacts Fabricated Assemblies Before Production – 1CUTFAB1cutfab.com · Accessed